
Dividing head
Enter the number of divisions or an angle and the calculator shows how many full crank turns to make and how many holes to count on which index plate circle. When simple indexing is impossible it suggests a differential setup.
2 + 12/54 turns + holes/circle
simple indexing- Crank turns
- 40/18 = 2.222
- Holes on circle
- 12 on the 54 circle
- Angle per division
- 20° 0′ 0″
Not sure about the numbers? An engineer will check the calculation and pick equipment from stock or to order.
Matching products
All dividing heads →
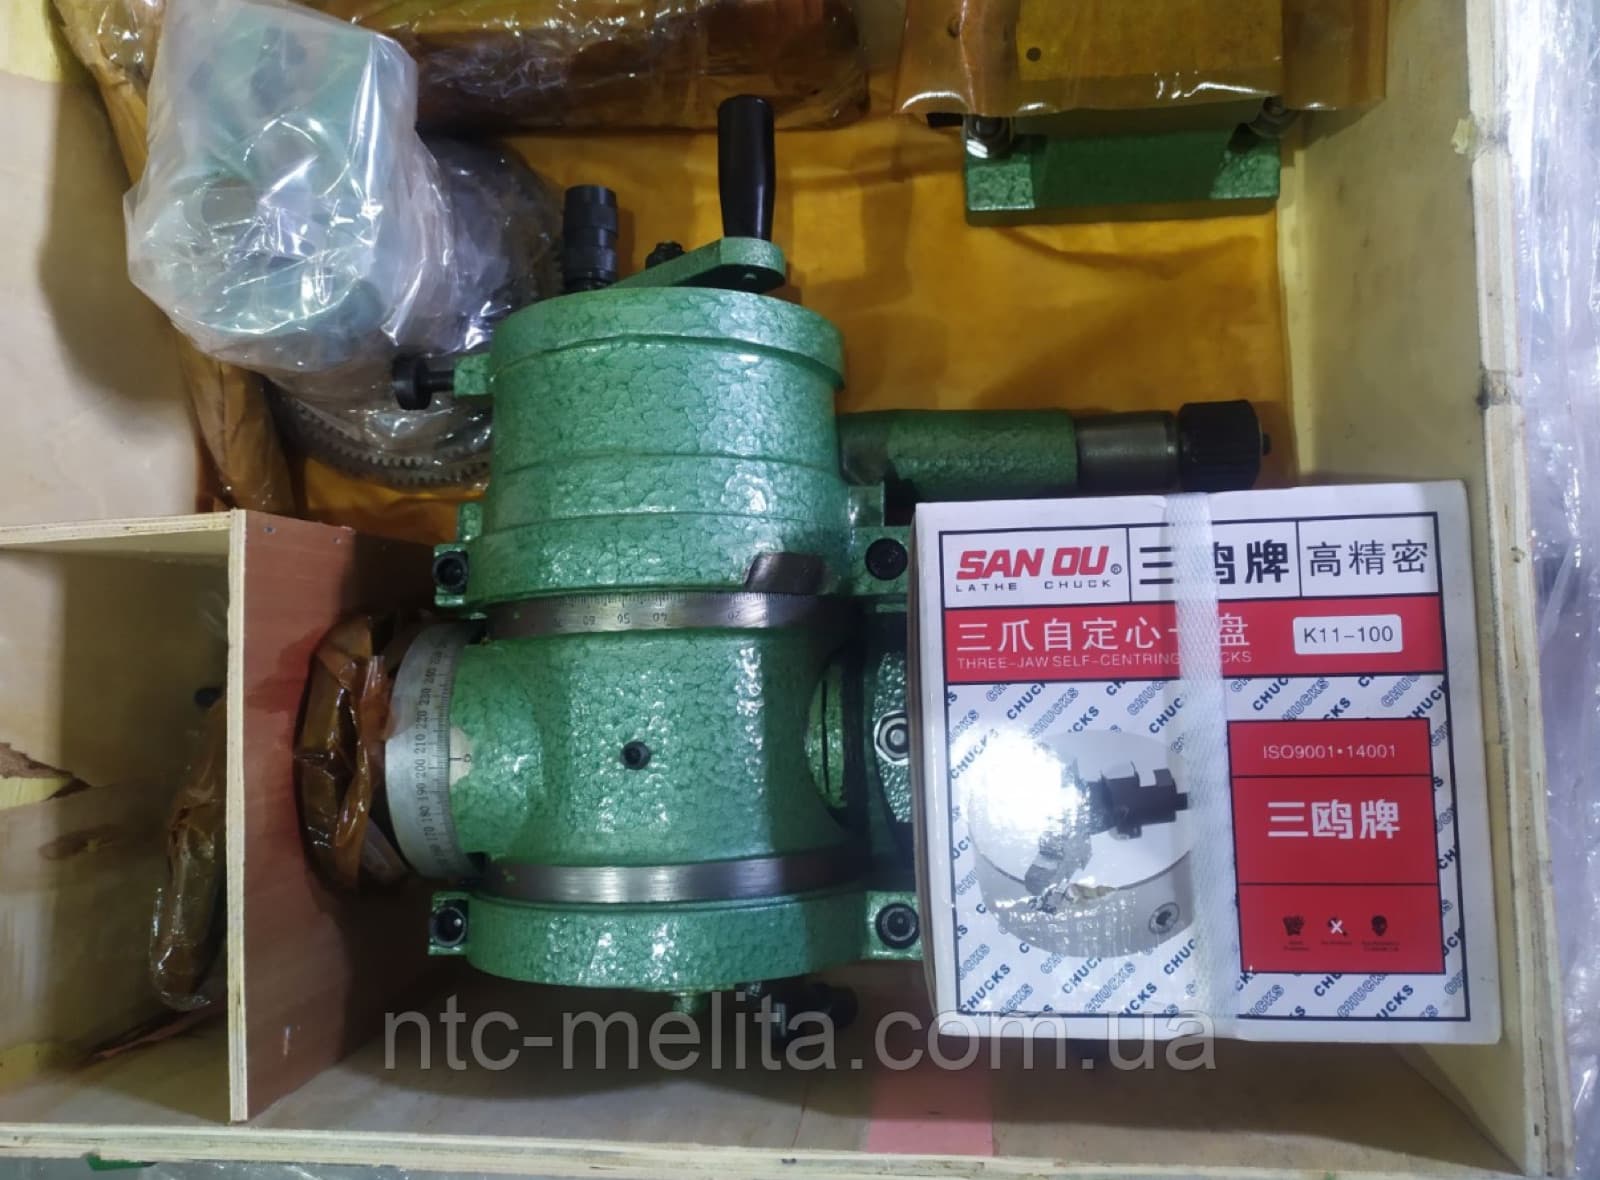
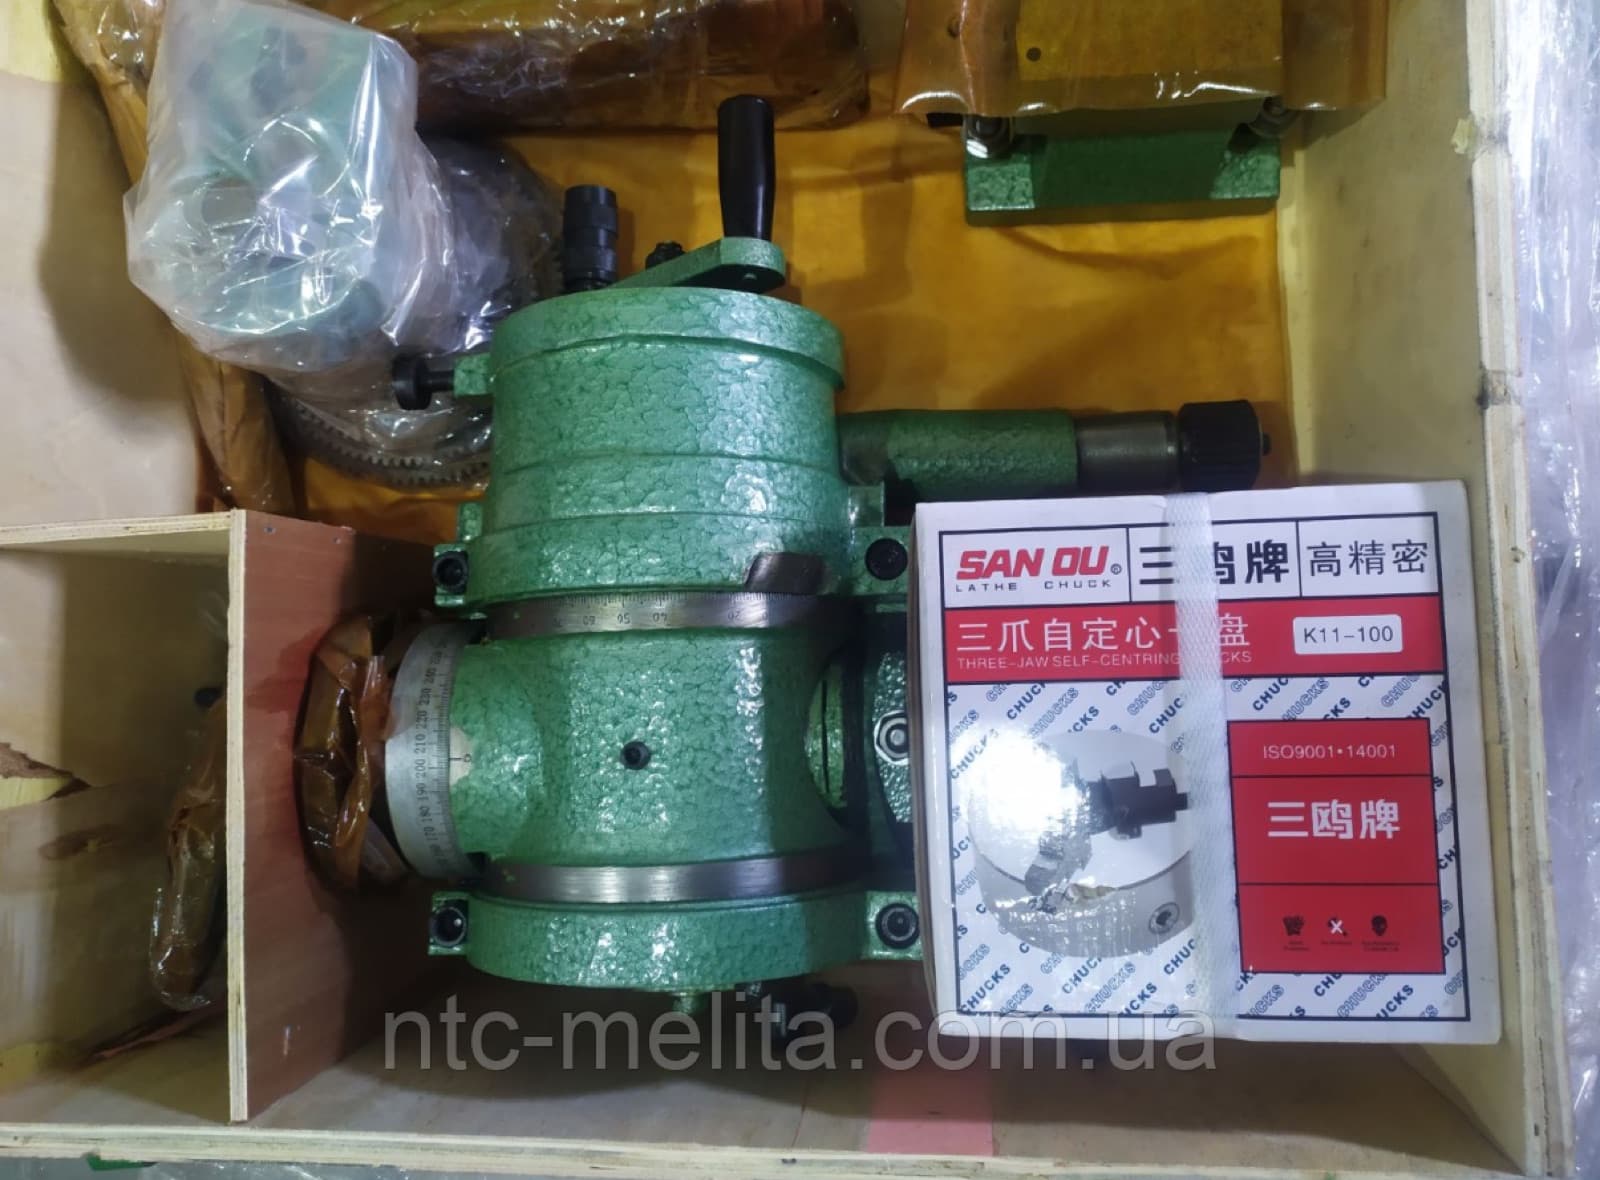
How it works
Most dividing heads have a 40:1 worm gear: 40 crank turns make one spindle revolution. 40 is the head ratio N stated in the manual. For Z divisions the crank turns n = N/Z.
The whole part is counted in full turns and the fraction is converted to a plate circle whose hole count is divisible by the denominator. For Z = 18: 40/18 = 2 2/9 = 2 and 12/54, i.e. two turns and 12 holes on the 54-hole circle.
For an angle, one crank turn moves the spindle 360/40 = 9°. 35° is 3 8/9 turns: 3 turns and 48 holes on the 54 circle. The calculator uses circles 16, 17, 19, 21, 23, 29, 30, 31, 33, 37, 39, 41, 43, 47, 49, 54 - check the plates of your own head first.
When differential indexing is needed
For primes such as 61, 67, 71 or 127 no circle fits. Take a nearby Z' that indexes simply, set the crank to N/Z' and gear the plate to the spindle with change gears of ratio i = N x (Z' - Z) / Z'. The sign gives the plate direction relative to the crank. The calculator finds the nearest Z' and computes i; take the actual gears from the head's set.
Common mistakes
- Counting the hole the plunger sits in. Set the sector arms to the number of spaces - one more hole is visible between them.
- Turning the crank back and forth. Always turn one way; if you overshoot, back off half a turn and come up again.
- Forgetting to lock the spindle before cutting.
- Using 40 for a head with a different ratio. Some imported heads are 60:1 or 90:1 - change N in the calculator.
Further reading
Head design, direct indexing and mistakes are covered in the article dividing head: index table and how to use it. UDG heads from D-160 to D-400 are in dividing heads.