Tap drill size
Pick the thread and pitch - the calculator gives the drill size for cutting and forming taps, the minimum blind hole depth and the thread profile depth.
Ø 8.5 mm drill
- For a forming tap
- 9.33 mm
- Blind hole depth
- ≥ 20 mm
- Thread profile depth
- 0.81 mm
Not sure about the numbers? An engineer will check the calculation and pick equipment from stock or to order.
Matching products
Drill presses →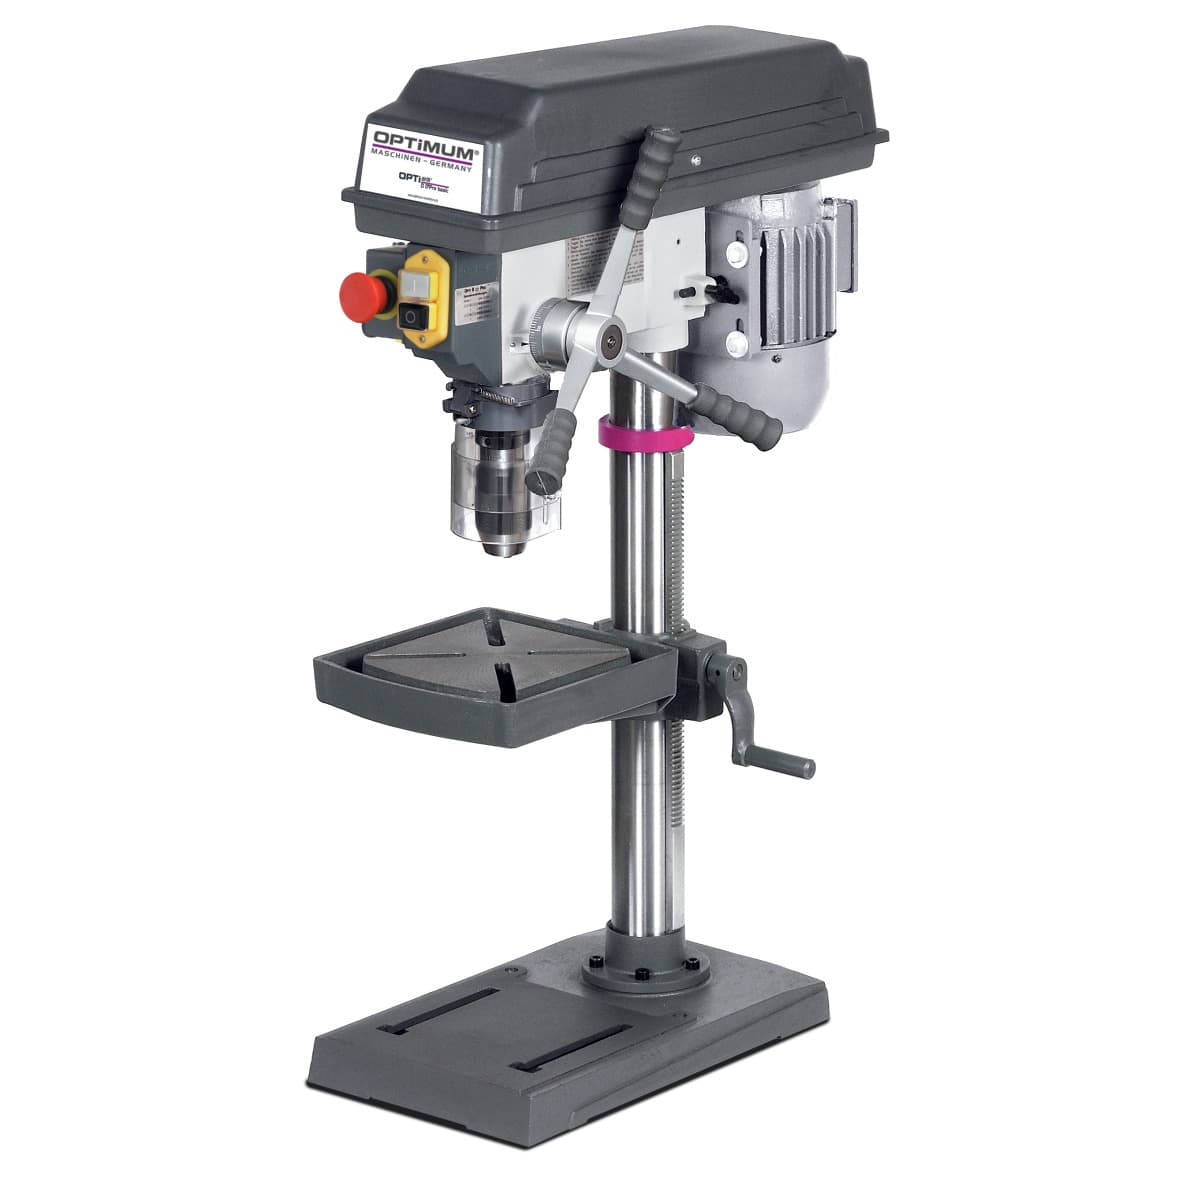
● In stockOPTIMUM B17Pro basic bench drill press
voltage230 Vweight36.5 kg
22 080 ₴incl. VAT · 18 400 ₴ excl. VAT

How it is calculated
For a cutting tap the drill diameter = D - P, where D is the nominal thread diameter and P is the pitch. M10 with 1.5 pitch: 10 - 1.5 = 8.5 mm. Fine pitches use the same formula: M10×1.25 - 8.75 mm, M10×1 - 9 mm, M12×1.5 - 10.5 mm, M12×1.25 - 10.75 mm, M16×1.5 - 14.5 mm, M20×1.5 - 18.5 mm, M24×2 - 22 mm.
A forming (roll) tap displaces metal instead of cutting it, so the hole is larger: about D - 0.45P. For M6 that is around 5.55 mm instead of 5 mm.
A blind hole should be at least 1.5D + 3P deep, so the tap chamfer has room and chips have somewhere to go. For M10: 15 + 4.5 = 19.5 mm. Thread profile depth is about 0.54P.
Tap drill chart for metric coarse threads
| Thread | Pitch, mm | Drill D - P, mm | In practice, mm |
|---|---|---|---|
| M3 | 0.5 | 2.5 | 2.5 |
| M4 | 0.7 | 3.3 | 3.3 |
| M5 | 0.8 | 4.2 | 4.2 |
| M6 | 1 | 5 | 5 |
| M8 | 1.25 | 6.75 | 6.8 |
| M10 | 1.5 | 8.5 | 8.5 |
| M12 | 1.75 | 10.25 | 10.2 |
| M14 | 2 | 12 | 12 |
| M16 | 2 | 14 | 14 |
| M18 | 2.5 | 15.5 | 15.5 |
| M20 | 2.5 | 17.5 | 17.5 |
| M22 | 2.5 | 19.5 | 19.5 |
| M24 | 3 | 21 | 21 |
| M27 | 3 | 24 | 24 |
| M30 | 3.5 | 26.5 | 26.5 |
| M36 | 4 | 32 | 32 |
| M42 | 4.5 | 37.5 | 37.5 |
| M48 | 5 | 43 | 43 |
Common mistakes
- A smaller drill to make the thread stronger - the tap is overloaded and breaks in the hole, while thread strength barely improves.
- A forming tap in a hole sized for a cutting tap breaks almost every time. Check the tap marking.
- A worn or wobbling drill makes the hole oversize and the thread incomplete. Check the hole with a caliper or plug gauge.
- In a blind hole the tap jams on chips - back it off every half turn and clear the chips.
- Work out drilling data with the speed and feed calculator and find a machine for the size in drill presses.