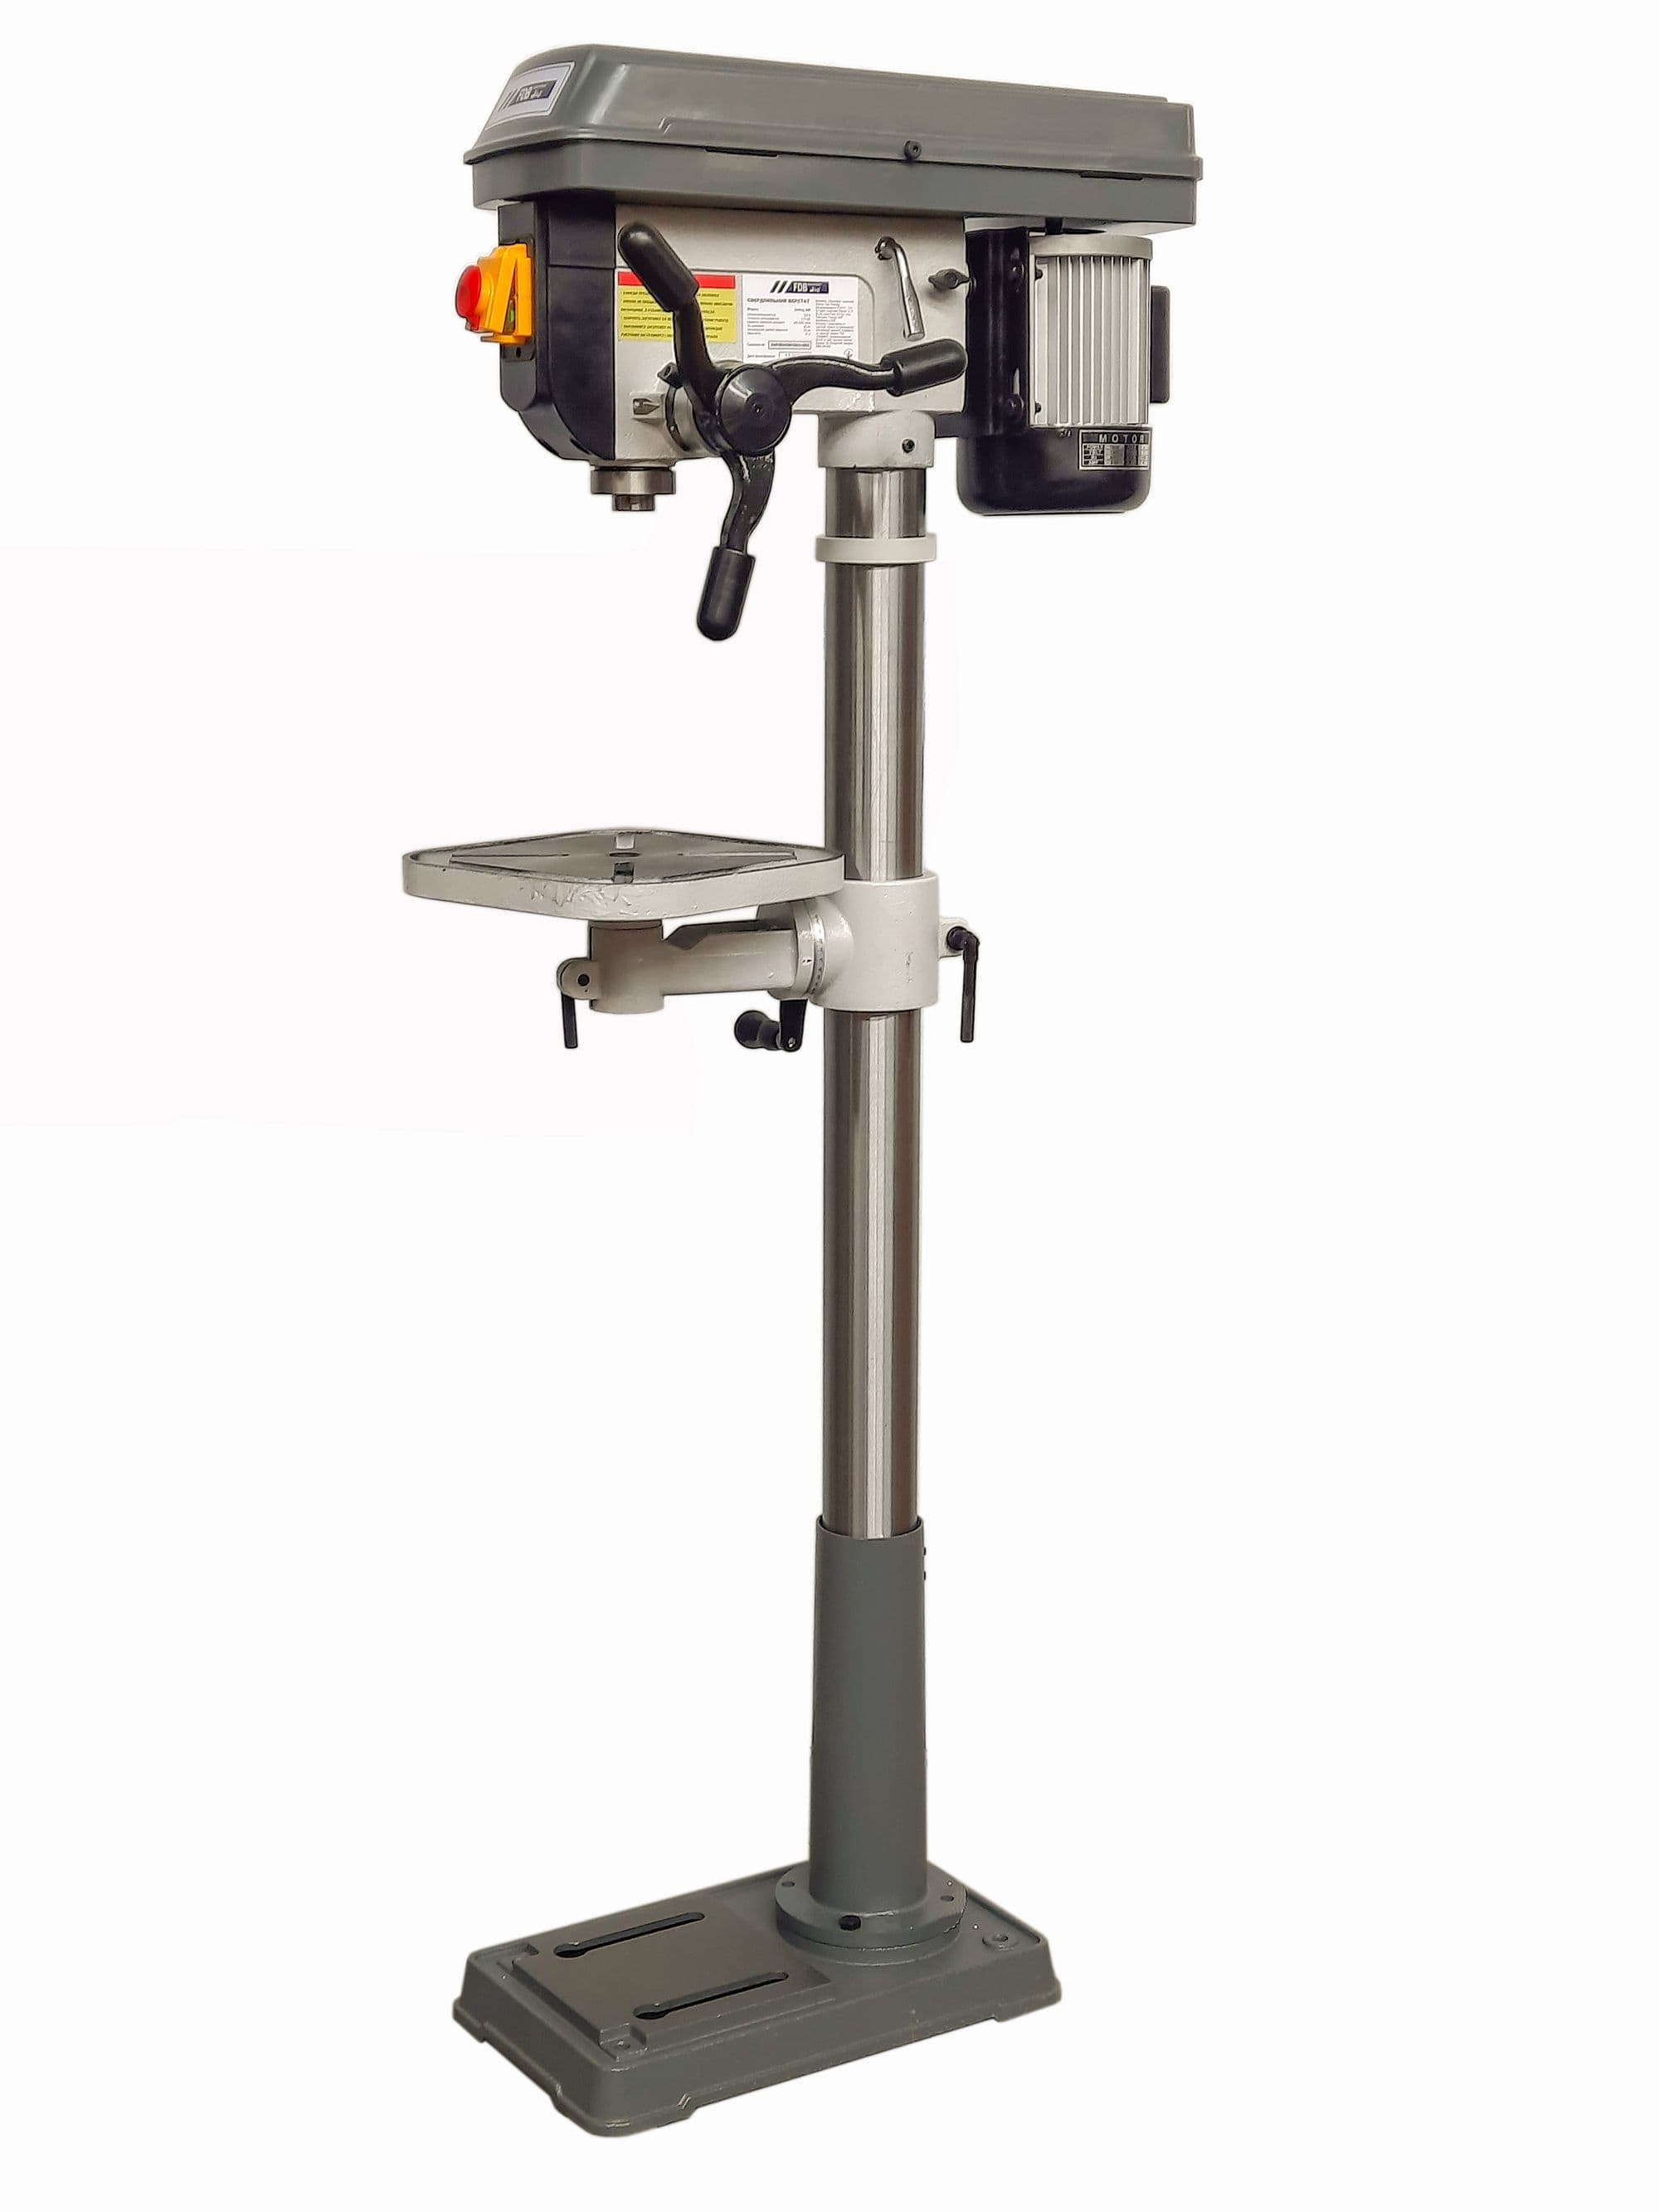
Drill press selector
Enter the largest hole you drill in steel and the part height - the calculator suggests the machine type, spindle taper, motor power and supply voltage.
Pillar (floor) drill
- Diameter with margin
- 22 mm
- Spindle taper
- МК3 / MT3
- Motor power
- 1.1-1.5 kW
Not sure about the numbers? An engineer will check the calculation and pick equipment from stock or to order.
Matching products
Compare all models →
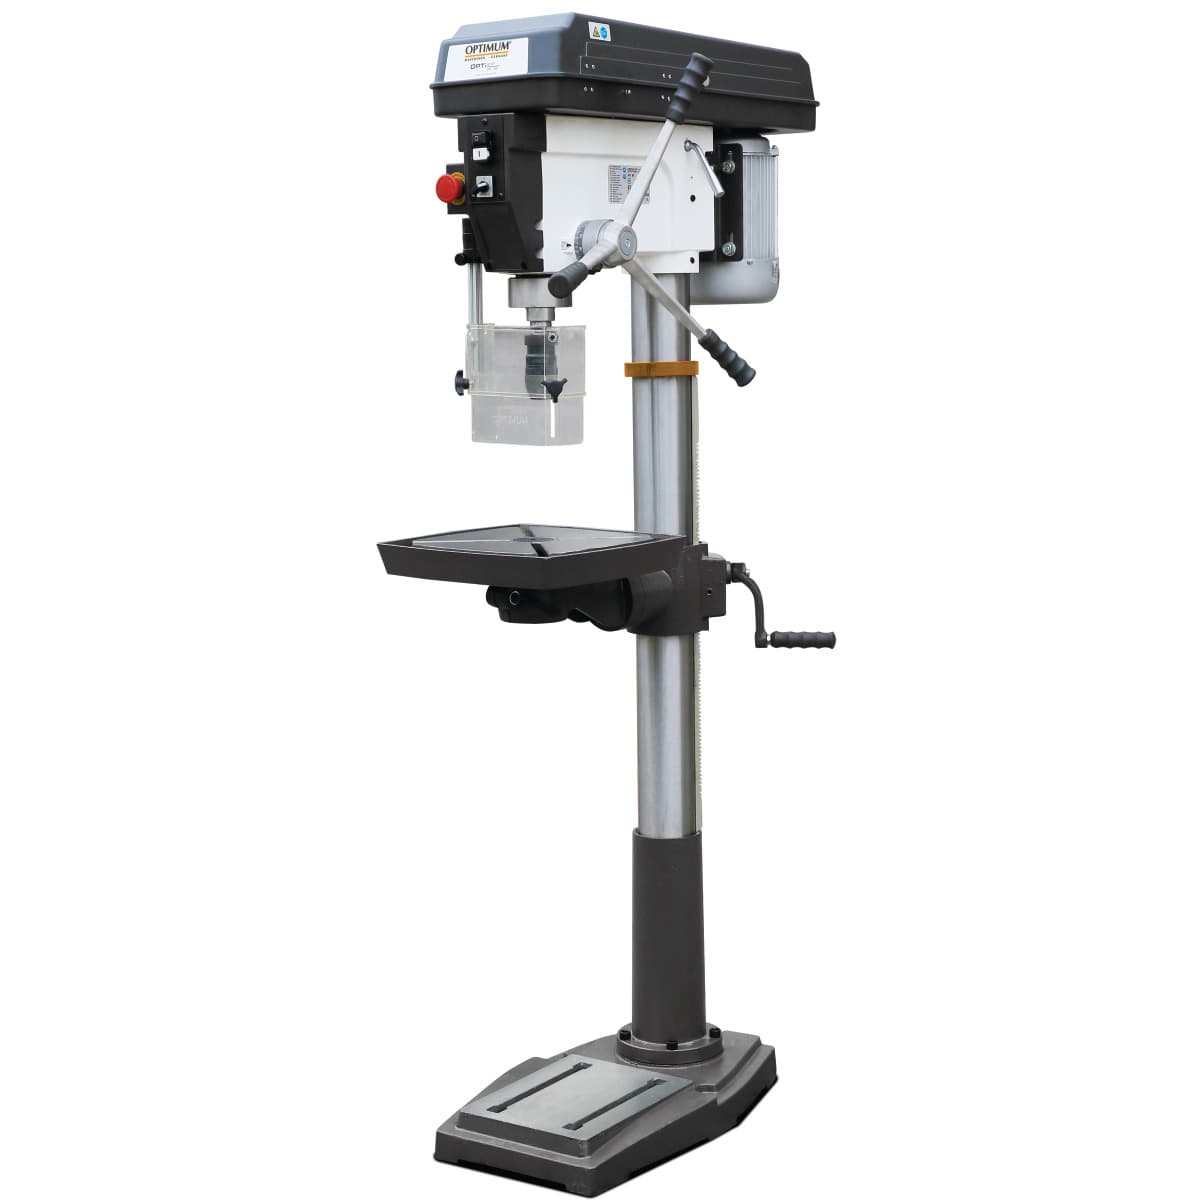
● In stockOptimum OPTIdrill DQ 32 Drill Press
power1.1 kWvoltage400 Vweight120 kg
56 280 ₴incl. VAT · 46 900 ₴ excl. VAT

How it is calculated
Take the largest drilling diameter in steel and add a 10-20% margin. The rated capacity of a drill press is given for structural steel at the limit, and daily work at the limit quickly wears out the spindle bearings and belt.
Machine type: benchtop if the diameter is up to 16 mm and the part is up to 300 mm high; pillar (floor) drill up to 35 mm and 600 mm; anything larger, or parts that are hard to move under the spindle, call for a radial drill.
The diameter then sets the spindle taper and motor power (table below). Supply: 230 V single phase for a workshop without three-phase power, 400 V three phase for a production shop; three-phase motors are simpler and pull more evenly under load.
Taper and power by drilling diameter
| Diameter in steel | Spindle taper | Motor power | Typical class |
|---|---|---|---|
| up to 16 mm | MT2 | 0.5-0.75 kW | benchtop |
| up to 32 mm | MT3 | 1.1-1.5 kW | pillar |
| over 32 mm | MT4 | from 2 kW | pillar or radial |
What else to check
- Throat (spindle axis to column) defines how far from the edge you can drill. For wide plates throat matters more than diameter.
- Quill travel: through holes in thick parts need travel at least equal to the thickness plus the drill point length.
- Lowest speed: large drills and core drills need 100-200 rpm. Work out cutting data with the speed and feed calculator.
- Tapping holes for M16-M20 in steel already needs a 25-32 mm class machine, not a 16 mm one.
- For a vise and large parts you need a table with T-slots, not just a round plate.
When to ask an engineer
If parts are heavy and awkward to move, or you need batch drilling with a jig or tapping on the machine, tell us what you drill and in which material. See benchtop drills, pillar drills and radial drills.