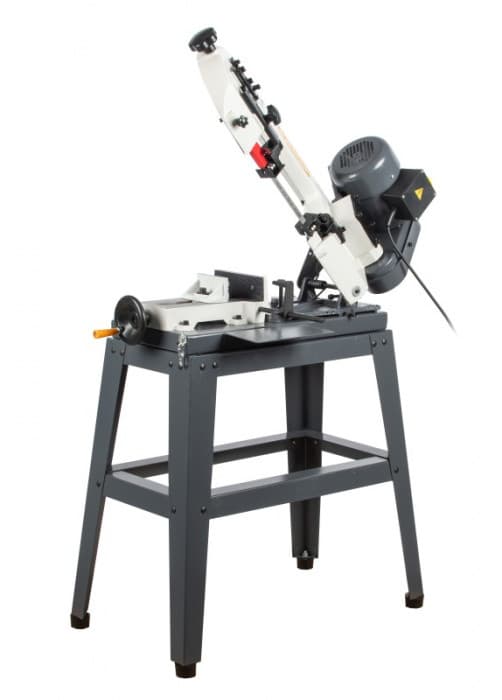
● In stockMetal-cutting band saw PPK-90U
voltage230 Vweight42 kg
21 840 ₴incl. VAT · 18 200 ₴ excl. VAT
Enter what you cut - solid bar, tube or profile, its size and material. The calculator returns the tooth pitch in TPI and the band speed in m/min.

The basic rule: 3-6 teeth should be in the cut at any moment. Fewer, and the teeth hit the edge and chip, especially on thin walls. More, and the gullets pack with chips, the blade stops cutting and starts to wander.
For solid stock the pitch is chosen by diameter or thickness; for tubes and profiles by wall thickness, because only the wall is in the cut.
Example: a 40×40 tube with a 2 mm wall takes 14/18, although the outer size alone would suggest 8/12 and the teeth would chip on the wall.
Pitch is given in TPI - teeth per inch. A 6/10 marking means variable pitch: the band alternates sections with 6 and 10 teeth per inch. Such a blade vibrates less and covers a wider size range than a constant pitch.
| Solid bar, diameter | TPI | Tube/profile, wall | TPI |
|---|---|---|---|
| up to 10 mm | 14/18 | up to 2 mm | 14/18 |
| up to 30 mm | 10/14 | up to 3 mm | 10/14 |
| up to 50 mm | 8/12 | up to 5 mm | 8/12 |
| up to 80 mm | 6/10 | up to 8 mm | 6/10 |
| up to 120 mm | 4/6 | over 8 mm | 5/8 |
| up to 200 mm | 3/4 | ||
| over 200 mm | 2/3 |
Approximate band speed: carbon steel 35-60 m/min, stainless 20-35 m/min, cast iron 30-45 m/min, aluminium 200-500 m/min. Many metal-cutting band saws have 2-4 fixed speeds - pick the nearest lower one.