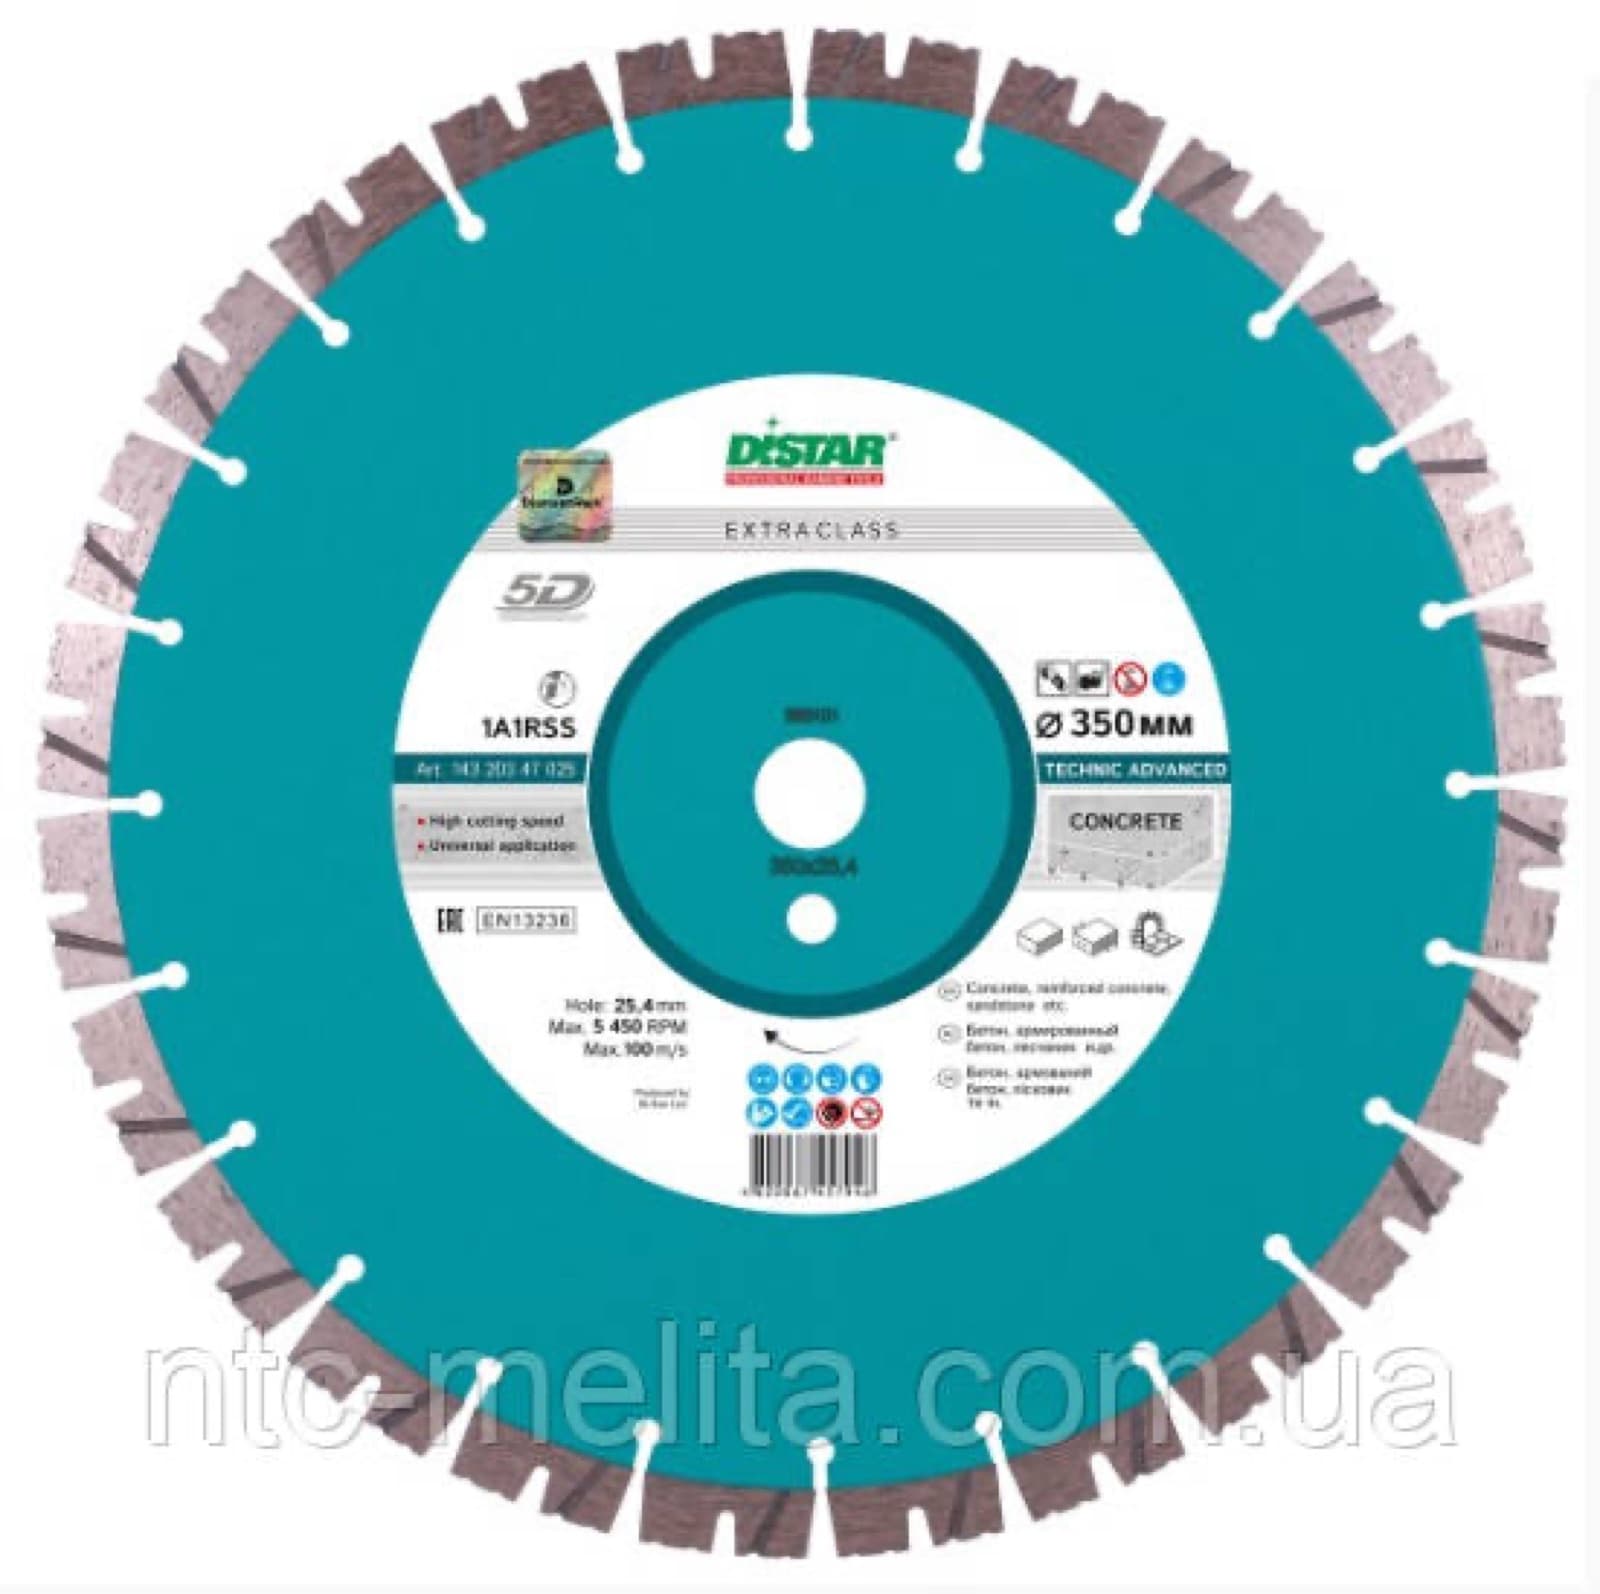
● In stockDiamond cutting disc 1A1RSS/C3 350x3.5/2.5x15x25.4-(11.5)-24-HIT Technic Advanced
5 260,80 ₴incl. VAT · 4 384 ₴ excl. VAT
DISTAR diamond blades for concrete in 300, 350, 400, 450, 500 and 600 mm for petrol cut-off saws and floor saws, mostly with a 25.4 mm bore. Segmented Classic H12, Meteor, Meteor H15, Sprinter Plus, Technic Advanced and Premier Active blades cut concrete, reinforced concrete and stone, and the Green Concrete series is for fresh, abrasive concrete. They cut dry in short passes or wet.




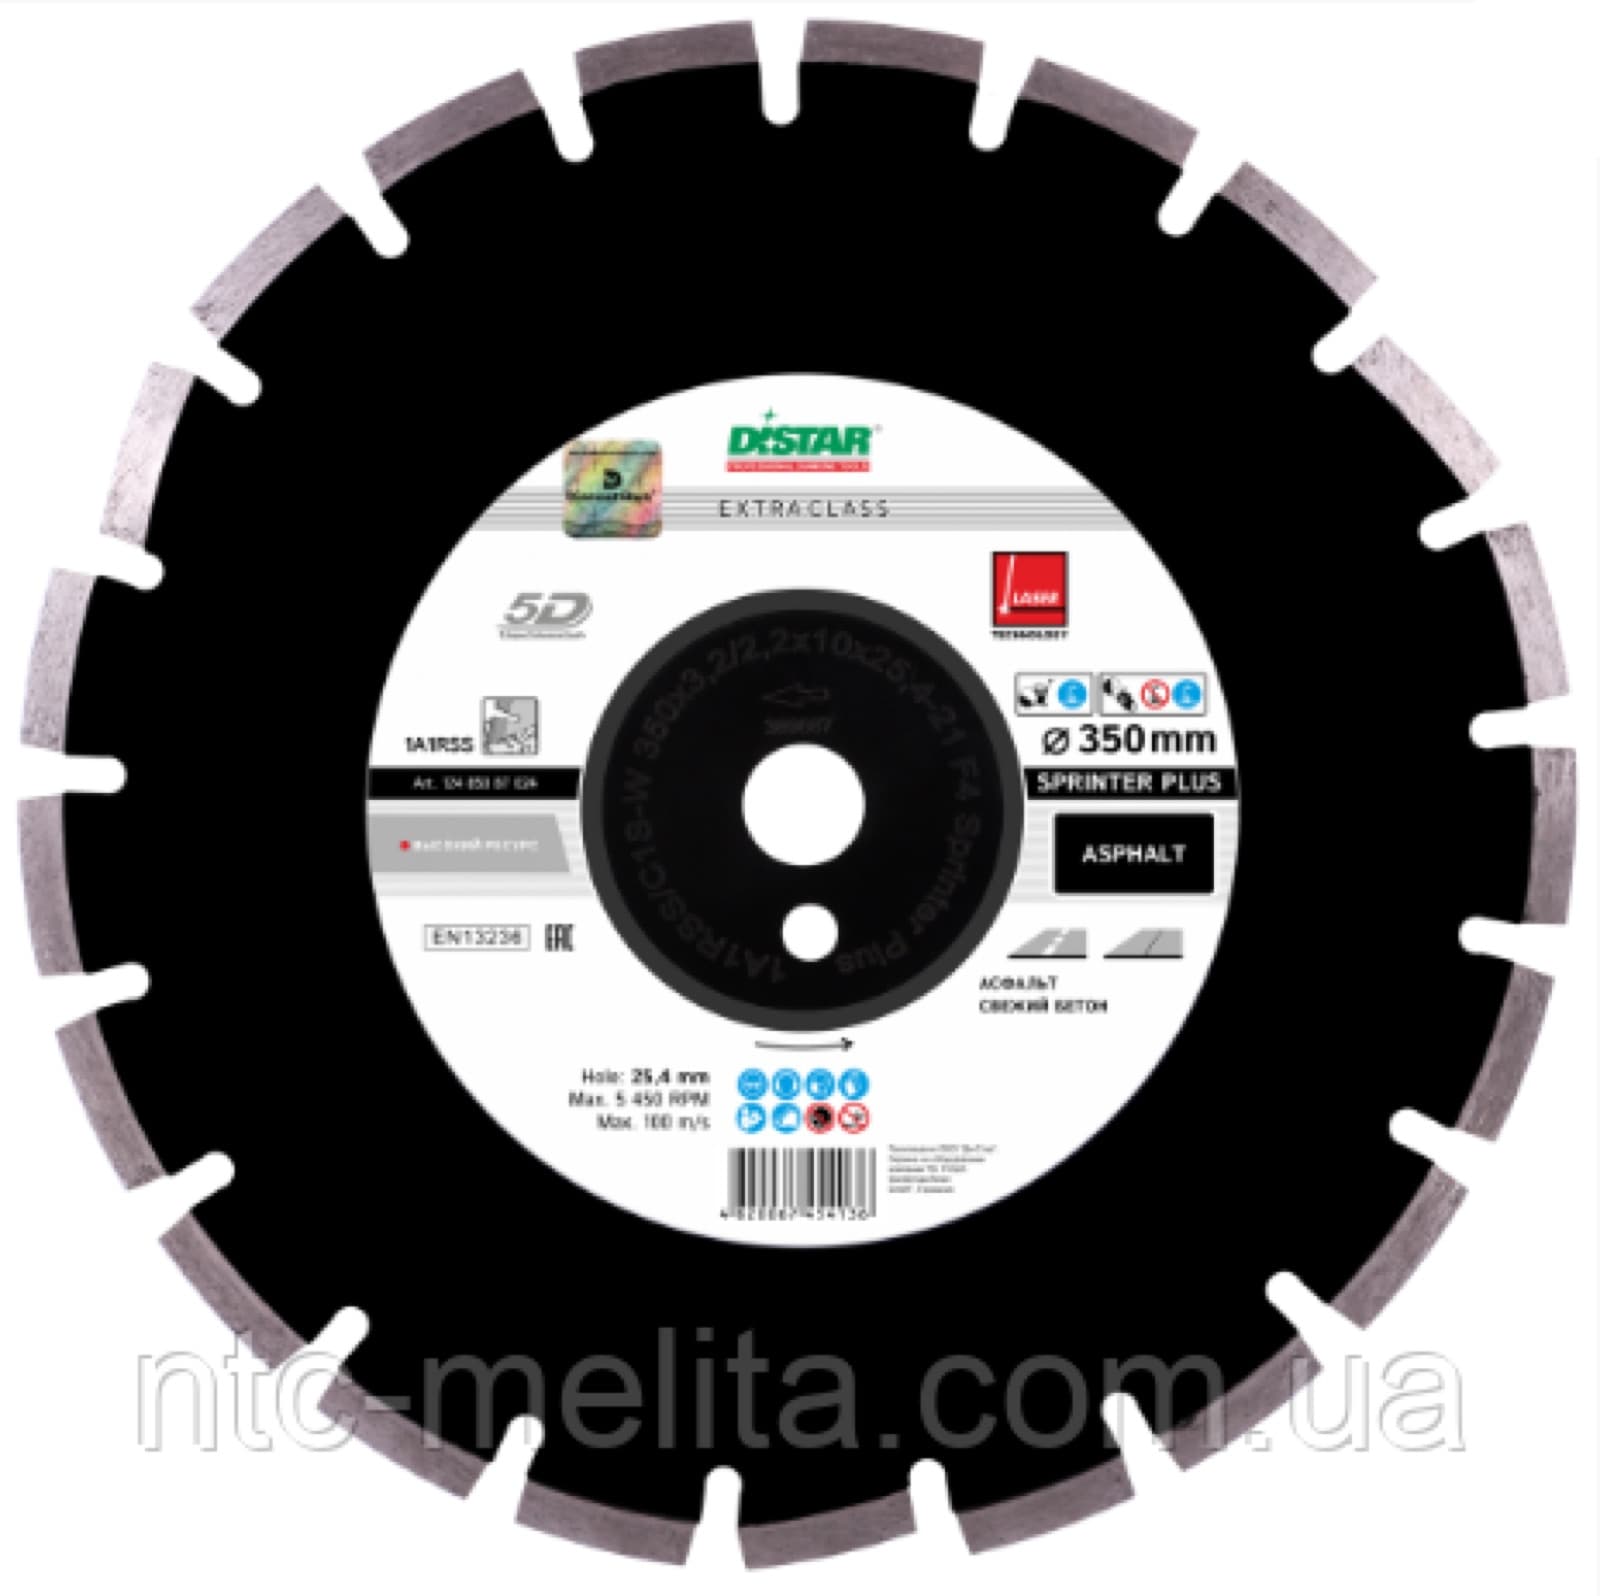


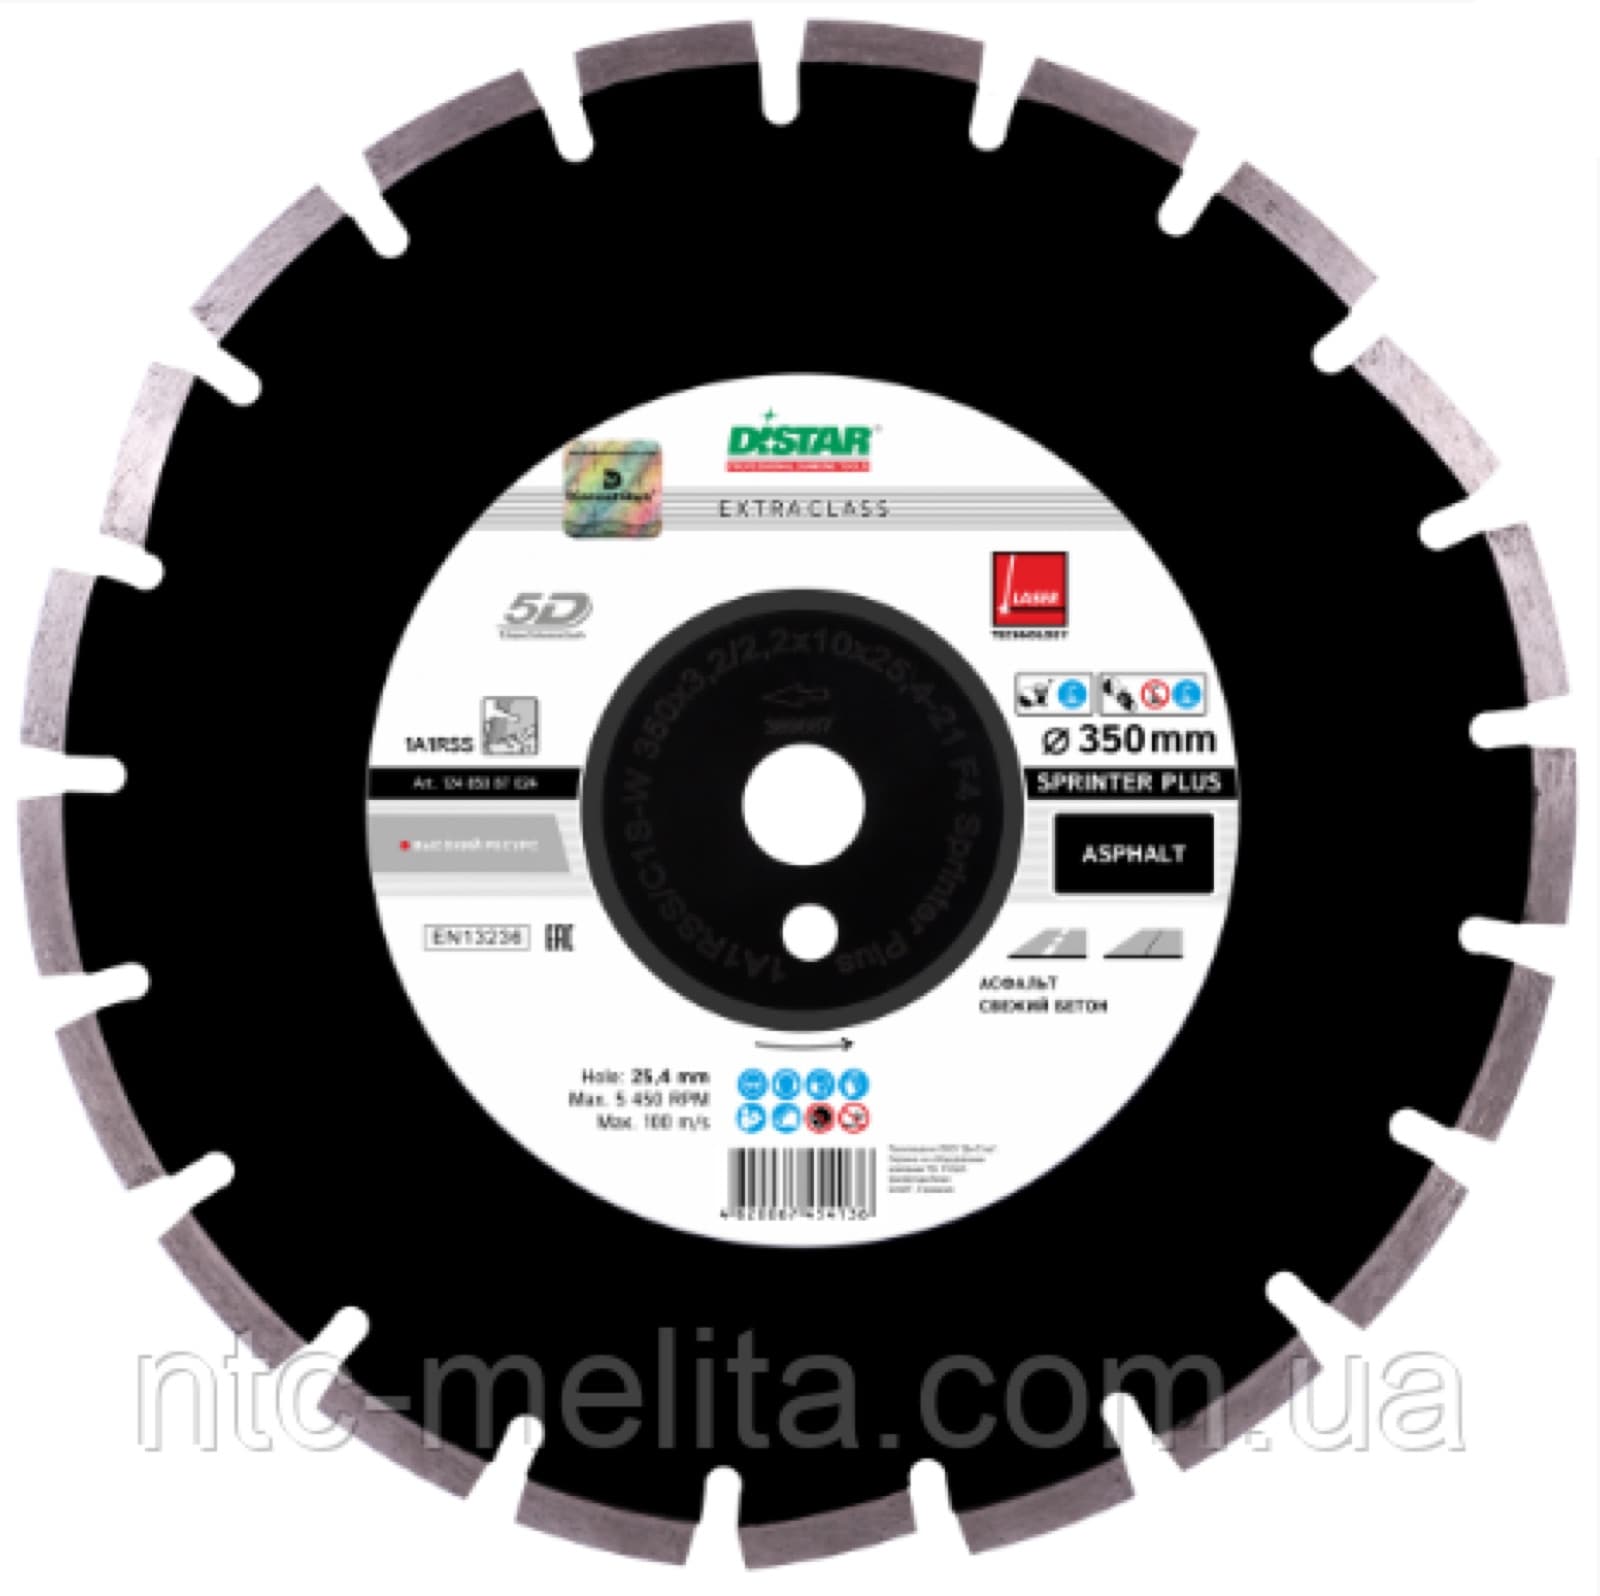
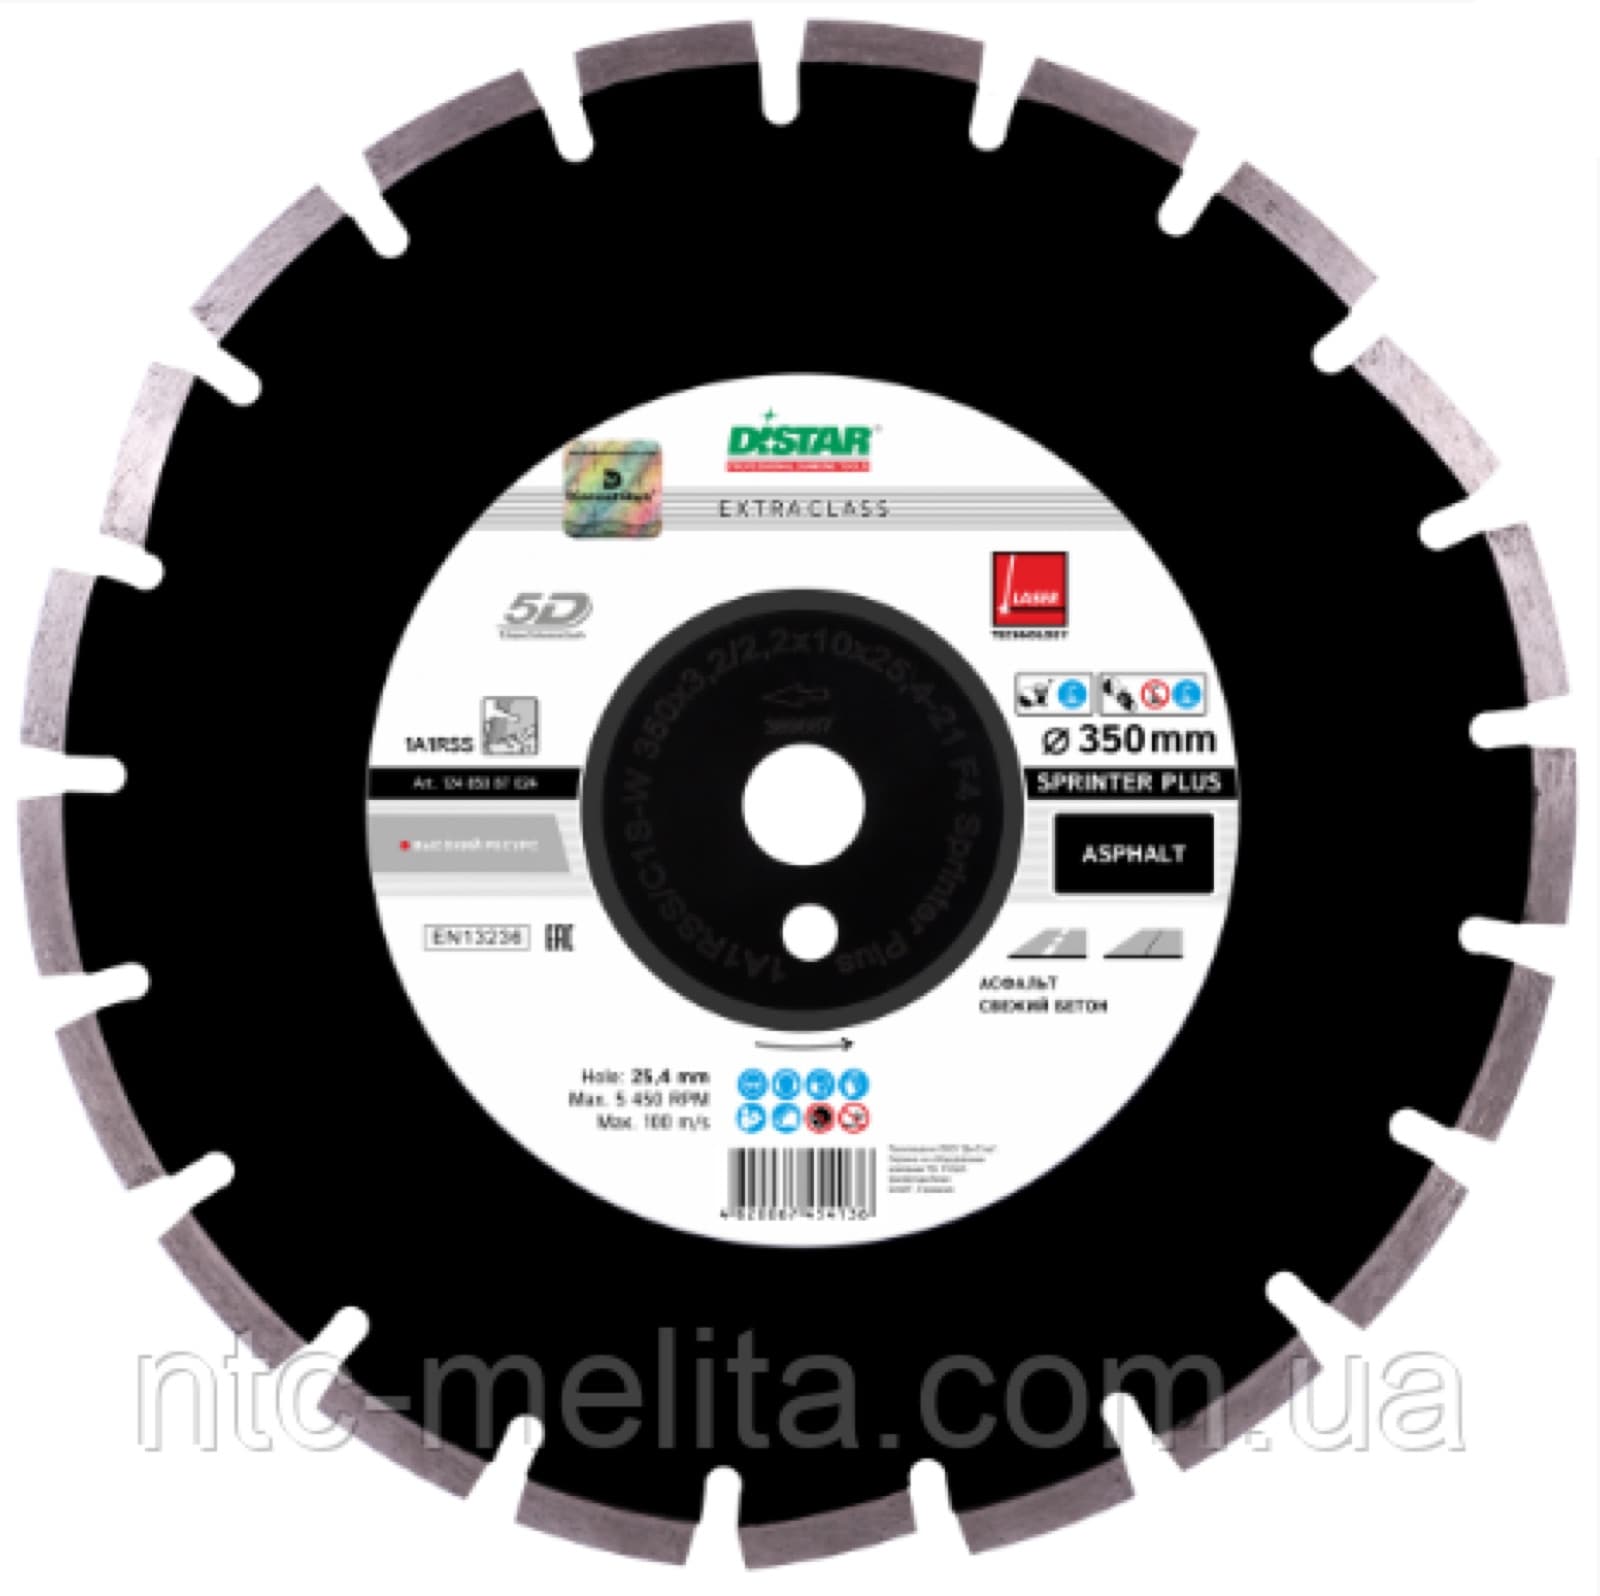


Cutting depth is roughly half the diameter minus the flange: a 350 mm blade on a petrol saw cuts about 120 mm, a 400 mm blade about 145 mm. Hand-held petrol saws usually take 300-400 mm, floor saws for slabs and road surfaces 400-600 mm. Choose no larger diameter than the machine guard allows and check the bore against the shaft: most blades here are 25.4 mm, one is 35 mm.
Service life depends on the height of the diamond layer. The titles state it as 10+2 or 13+2 mm, and the H12 or H15 mark in the Classic and Meteor series means a total segment height of 12 or 15 mm, so these blades last longer. Narrow gullets between segments clear slurry and cool the blade, which is why segmented blades suit long cuts. More segments on the same diameter mean less vibration and a cleaner cut.
Reinforced concrete needs a blade that cuts both concrete and rebar without burning the segments, so such series use harder diamonds and stronger segment bonding. Asphalt and green concrete are highly abrasive and call for a hard bond and undercut protection of the core. Old dense concrete and granite cut better with a softer bond that does not glaze.
On floor saws the blades run with water feed, which cools the segments, flushes slurry and reduces dust. A petrol saw can cut dry in short passes, letting the blade cool at idle between them. Blue spots on the core show overheating: such a blade loses tension and may wobble. Do not force the feed: the blade should cut under the weight of the machine, not operator pressure, so the segments wear evenly.