
Metal-cutting band saw OPTIsaw S275NV vario
5Reviews: 1power1.5 kWvoltage230 Vweight185 kg
125 280 ₴incl. VAT
104 400 ₴ excl. VAT · invoice for companies and sole proprietorsGet an invoice or a quote
Nova Poshta, Meestat the carrier's rate
Freight carrierat the carrier's rate
Pickup, Dniprofree
Specifications
| Main | |
|---|---|
| Manufacturer | Optimum |
| Country of origin | Germany |
| Blade speed | 20 - 90 m/min |
| Band saw blade length | 2480 mm |
| Band saw blade width | 27 mm |
| Band saw blade thickness | 0.9 mm |
| Cutting angle | 0 - 60° |
| Feed | variable control |
| Saw frame lift | manual |
| Dimensions and weight | |
| Length | 1400 mm |
| Width | 685 mm |
| Weight | 185 kg |
| Electrical | |
| Motor power | 1.5 kW |
| Coolant pump power | 0.090 kW |
| Voltage | 230 V |
| Frequency | 50 Hz |
| Cutting | |
| Cutting 0°, round | 225 mm |
| Cutting 0°, square | 190 mm |
| Cutting 0°, rectangle, flat | 150 x 245 mm |
| Cutting 45°, round | 145 mm |
| Cutting 45°, square | 150 mm |
| Cutting 45°, rectangle, flat | 190 x 150 mm |
| Cutting 60°, round | 90 mm |
| Cutting 60°, square | 90 mm |
| Cutting 60°, rectangle, flat | 120 x 90 mm |
Description
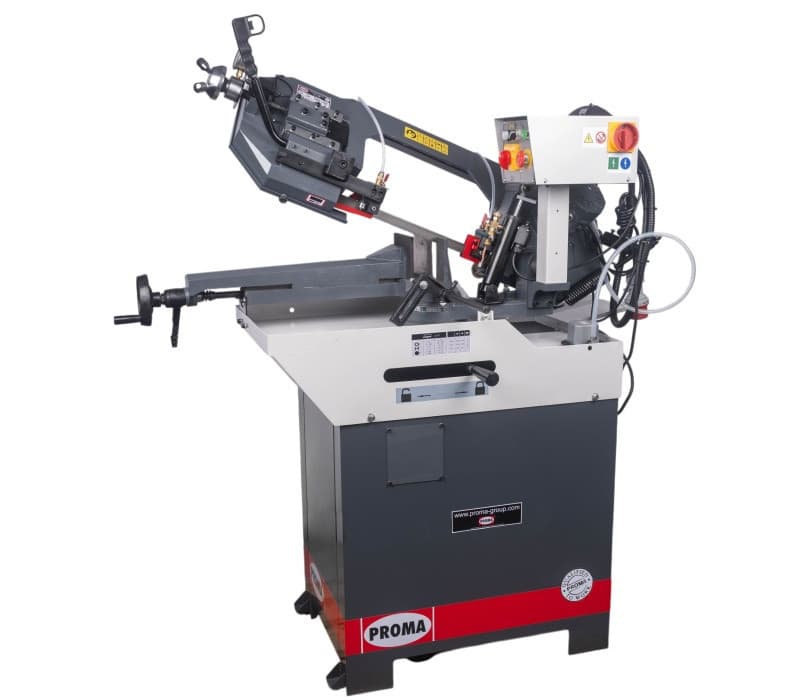
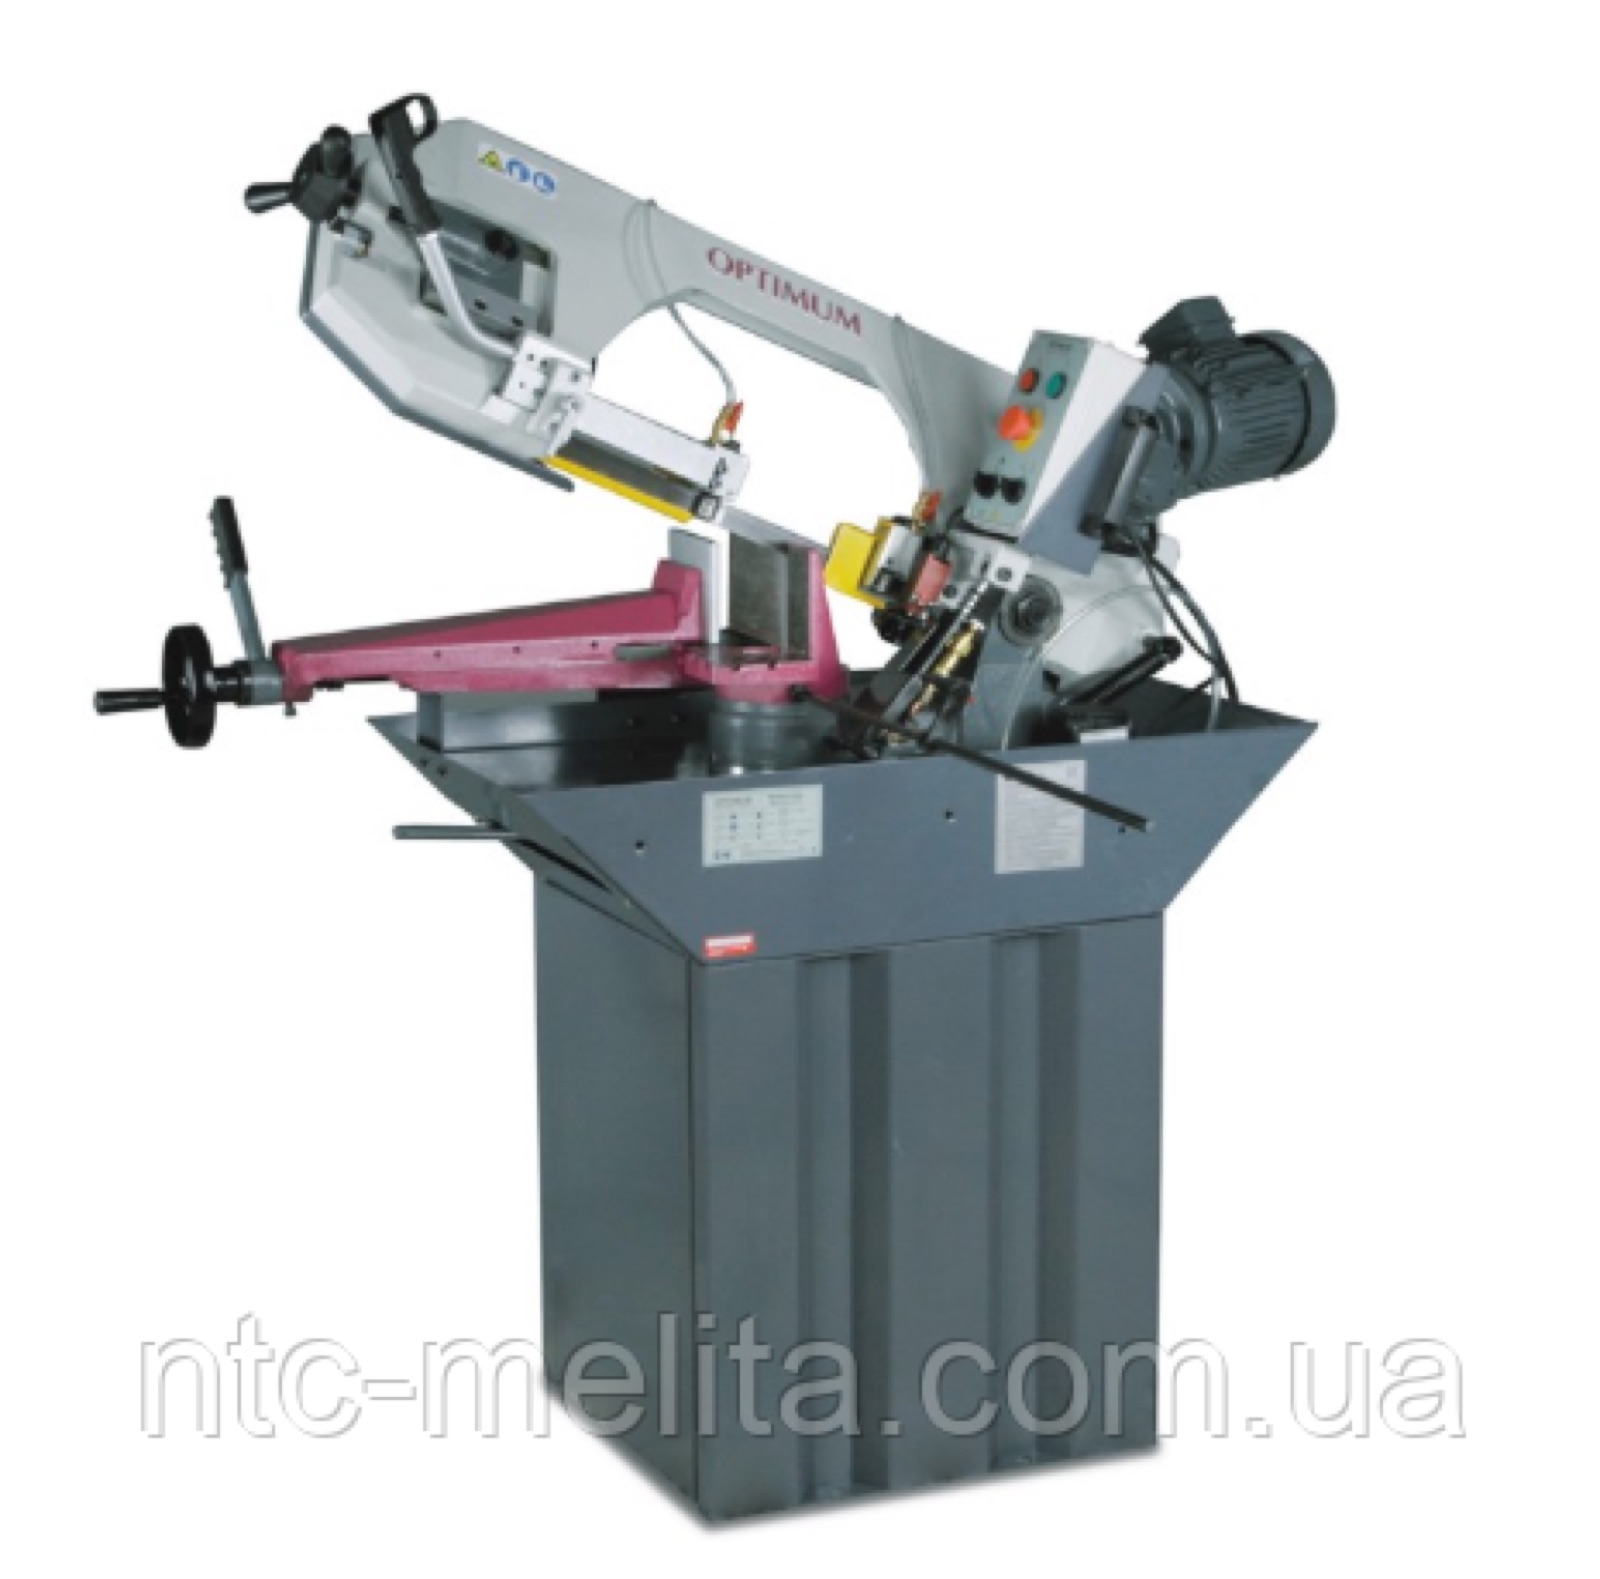
The OPTIsaw S275NV Vario metal band saw cuts round and profiled stock, pipe and solid workpieces in steel, aluminium and non-ferrous metals. Smooth hydraulic frame feed and blade cooling give a straight cut without overheating, so this band saw machine is well suited to cutting batches of identical blanks to length.
Maximum cut at 90° is 225 mm round or 245 x 180 mm rectangular, 160 mm at 45° and 100 mm at 60°. The 1.5 kW motor runs on 220 V, the variator gives stepless band speed of 20-90 m/min, the blade is 2480 x 27 x 0.9 mm and the machine weighs 200 kg. It is built for machine shops, stock-cutting areas and metal depots doing one-off and small-batch cutting.
The OPTIsaw S275N is the most in-demand and most popular metal-cutting band saw in the entire band saw range of the Optimum brand.
This popularity was the Optimum OPTIsaw S275N metal-cutting band saw has earned for good reason.
Technical description:
- High build quality, ease of use and a moderate price are its main advantages.
- Swivelling the saw frame up to 60° allows the cutting angle to be changed quickly and easily with almost no loss of working time, while maintaining high cutting accuracy with no saw vibration whatsoever.
- Structural rigidity and cutting accuracy are ensured by the heavy cast iron frame.
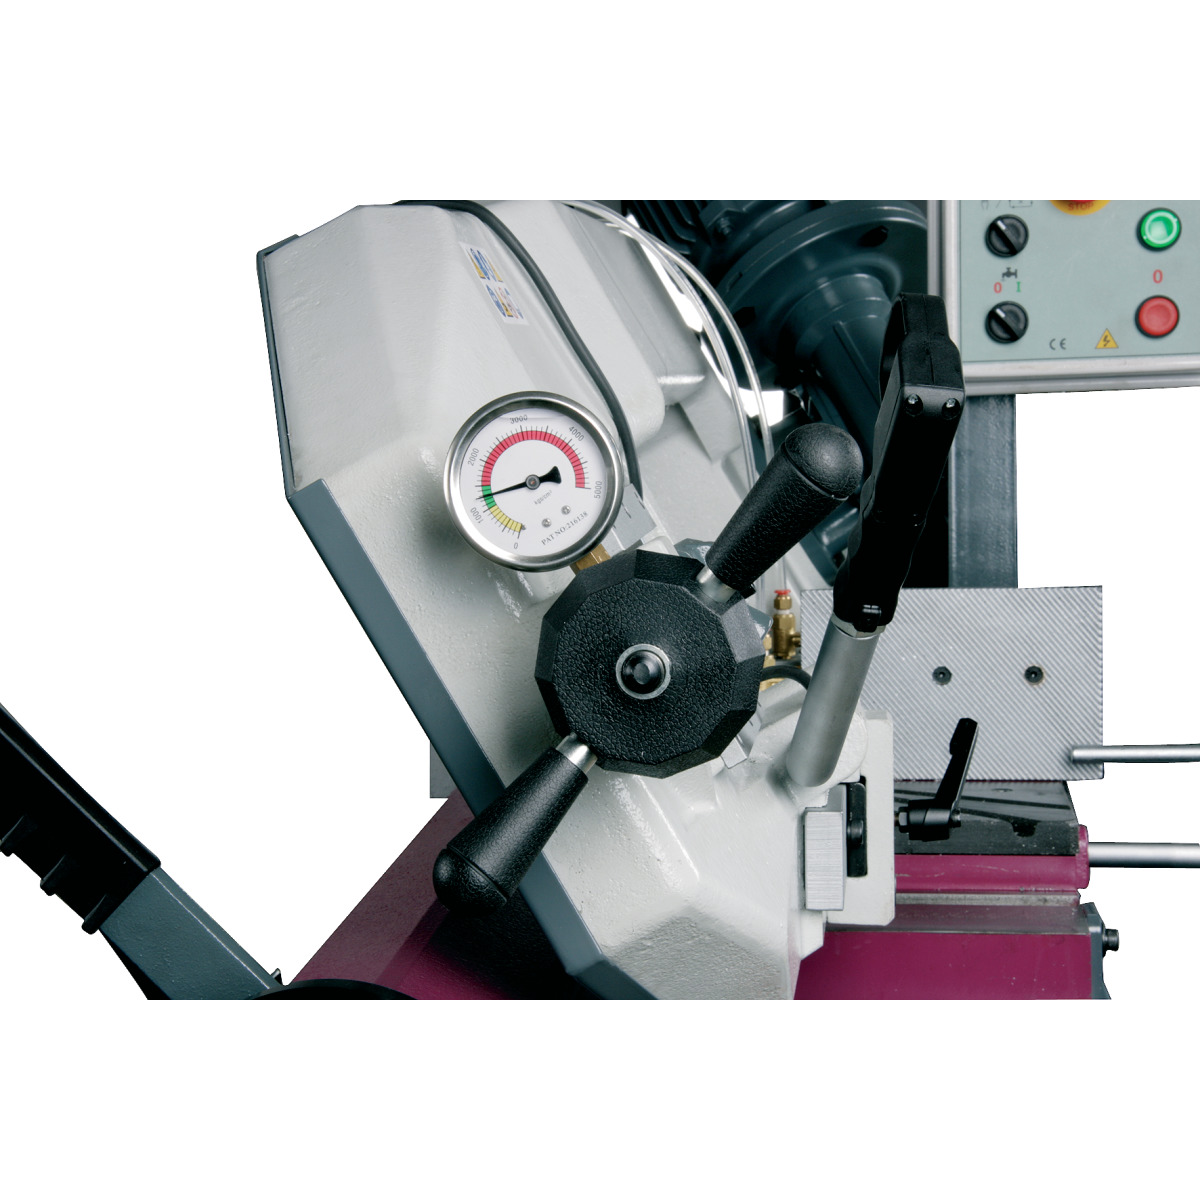
- Smooth lowering of the saw frame during cutting is achieved by a correctly matched counterweight and the flawless operation of the band saw's hydraulic cylinder.
- At the end of the cut, the automatic limit switch trips and the saw frame returns to its initial position.
- For accurate cuts, five pairs of roller guides keep the saw blade on its set path.
- The coolant system delivers coolant precisely to the cutting zone, effectively cooling the blade and flushing away metal chips.
- The two-speed motor on the OPTIsaw S 275N metal-cutting band saw allows cutting at 45/90 m/s, while on the OPTIsaw S275N Vario, thanks to the variator, cutting speed is steplessly adjustable from 20 to 90 m/s.
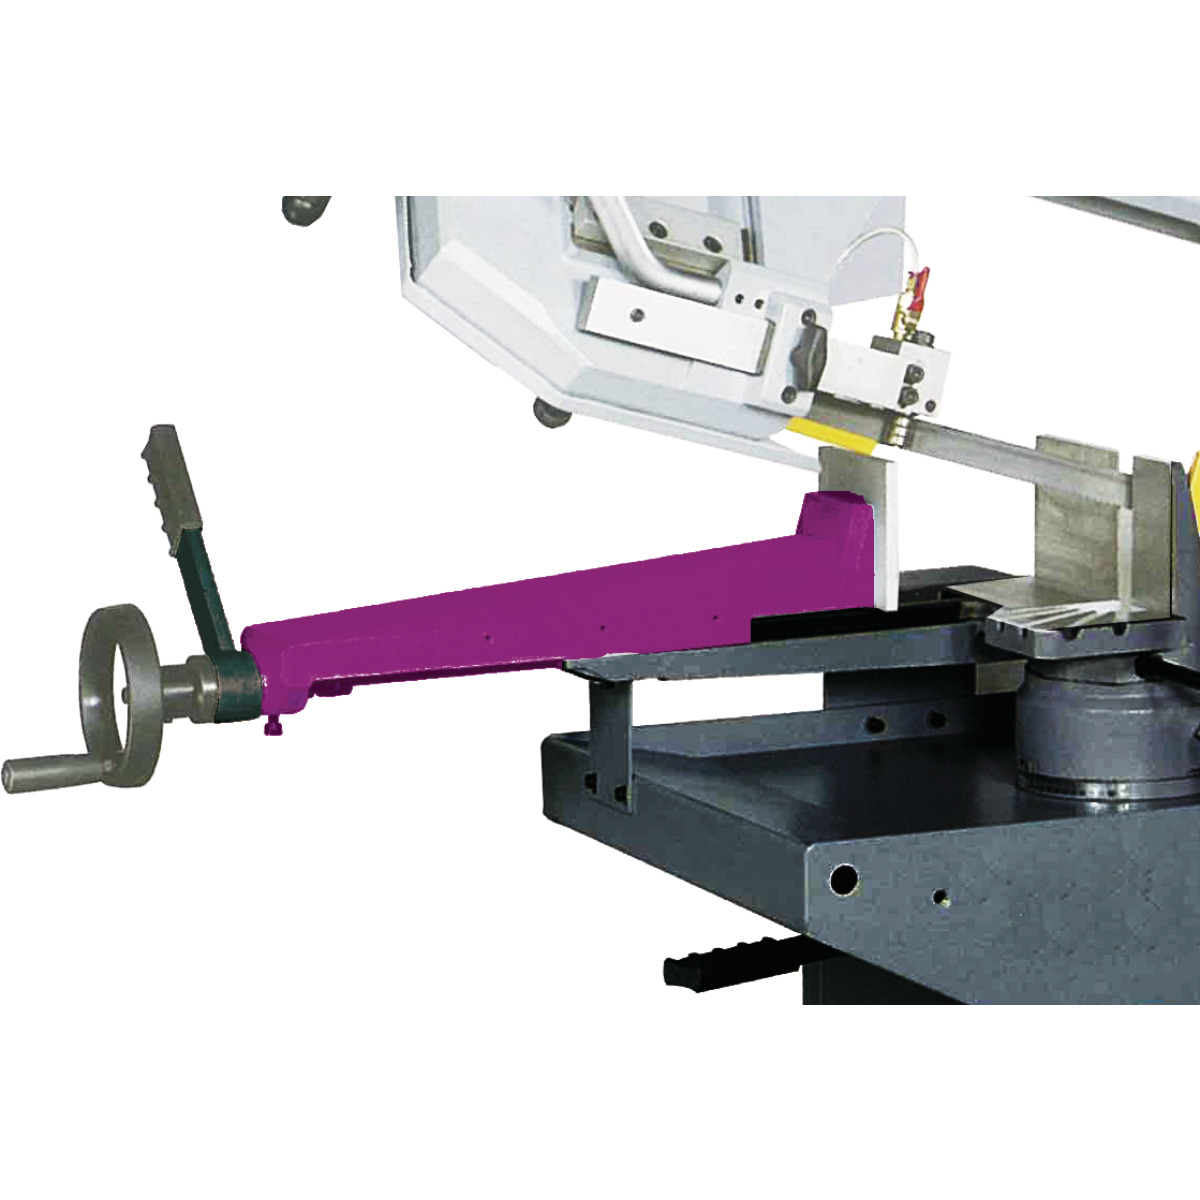
- The quick-clamping vise allows a large volume of work without losing time when changing workpieces. This is especially important when making many identical cuts.
- Particularly worth noting is the comfort of working with the band saw: a simple, convenient control panel, quiet operation and a blade tensioning system that even a "beginner" understands are the keys to the popularity of the Optimum band saw.
Main features: |
|
| Quick-clamping vise. | Feed rate adjustment with a back-pressure hydraulic cylinder. |
Specifications: |
||
| Band saw model | OPTIsawS 275N | OPTIsawS 275NV Vario |
| Item No. | 3300260 | 3300265 |
| Power supply | ||
| Motor | 1.1 kW / 380 V | 1.5 kW / 220 V |
| Coolant pump | 40 W | 50 W |
| Machine data | ||
| Max. cutting diameter, round stock, 90°, mm | 225 | |
| Max. cutting size, rectangular stock, 90°, mm | 245 x 180 | |
| Max. cutting diameter, round stock, 45°, mm | 160 | |
| Max. cutting size, rectangular stock, 45°, mm | 160 x 160 | |
| Max. cutting diameter, round stock, 60°, mm | 100 | |
| Max. cutting size, rectangular stock, 60°, mm | 100 x 100 | |
| Saw blade size, mm | 2480 x 27 x 0.9 | |
| Cutting speed, m/min | 45 / 90 | 20 — 90 stepless |
| Overall dimensions | ||
| Length with vise closed, mm | 1360 | |
| Length with vise open, mm | 1630 | |
| Width without workpiece stop | 510 | |
| Width with workpiece stop | 1140 | |
| Height in lowest position | 1420 | |
| Height in highest position | 1690 | |
| Machine weight, kg | 185 | 200 |
Scope of delivery:
- Bimetal saw blade.
- Workpiece stop.
- Quick-clamping vise.
- Machine stand.
- Limit switch.
- Operating manual in Russian.
| OPTIONAL ACCESSORIES | ITEM NO. | ||
|---|---|---|---|
| Roller conveyor MSR4 | 3357610 | ||
| Roller conveyor MSR7 | 3357611 | ||
| Roller conveyor MSR10 | 3357613 | ||
Metal-cutting band sawswith similar specifications are available from Proma (Proma PPS 220), Zenitech (Zenitech BS 225, Zenitech BS 220), JET (JET HBS-916W, JET HVBS-912,JET MBS-910CS), FDB machinen (FDB SG260HD, FDB SG 5020).
Each of the models listed above deserves attention, but the OPTIsaw S 275N metal-cutting band saw, and especially the OPTIsaw S 275NV vario, compare favourably with competitors. Some competing models are much more expensive than the OPTIsawS 275G, others have weak (fragile) assemblies, others lack a swivelling saw head or vise, and some fall short on cutting accuracy. Cutting accuracy, reliability and ease of use, a quick-clamping vise and a speed variator combined with a reasonable price are the factors behind the market success and popularity of the OPTIsaw S 275N and S 275NV vario.
Recommended band saw cutting parameters.- Clamping workpieces
Clamp workpieces so as to eliminate blade vibration as far as possible. This increases productivity and tool life.
In some cases, when cutting a bundle of workpieces, it may be advisable to tack-weld the workpieces together
- Cooling
Active cooling of the cutting zone with coolant helps avoid overheating of the tool and workpiece and clears chips from the cutting zone. Coolant emulsion is usually used when cutting steel; cast iron is most often cut without it (dry). Coolant is most effective when cutting structural, tool and alloy steels, titanium and nickel alloys. - Cutting speed and feed
Cutting speed depends on the hardness, type and cross-section of the workpiece. The stronger the workpiece material, the lower the cutting speed should be. Workpieces with a smaller cross-section can be cut faster than those with a large cross-section. Tubes and profiles are cut at low speed, and a constant feed is very important. If vibration occurs, change the cutting speed up or down by the smallest possible amount. As the tool dulls, the feed is increased.
| Steel grade | Cutting speed, m/min (M42) |
| Structural / free-cutting | 80 — 90 |
| Heat-treatable | 45 — 75 |
| Unalloyed tool / bearing | 40 — 60 |
| Alloyed tool / high-speed | 30 — 40 |
| Stainless | 20 — 35 |
| Heat-resistant | 15 — 25 |
| Table for checking cutting parameters by the type of chips produced | |
| Fine or powdery chips — increase the feed | |
| Loosely curled chips — the cutting speed is set correctly | |
| Thick, heavy or blue chips — the cutting speed is too high | |
- Tooth pitch
Blades with variable tooth pitch 1.5/2, 2/3, 3/4, 4/5, 4/6, 5/6 and a 10° rake angle are best for cutting solid workpieces of high-quality high-alloy steels and produce long chips. For such workpieces these blades give the cleanest, highest-quality cut.
For tubes with a wall thickness of up to 8 mm, blades with a 0° rake angle give the best results.
| Recommended tooth pitch for solid workpieces | |||
| Constant tooth pitch | Variable tooth pitch | ||
| Workpiece cross-section, mm | Tooth pitch, Z | Workpiece cross-section, mm | Tooth pitch, Z |
| up to 10 | 14 | up to 25 | 10 / 14 |
| 10 — 30 | 10 | 15 — 40 | 8 / 12 |
| 30 — 50 | 8 | 25 — 50 | 6 / 10 |
| 50 — 80 | 6 | 35 — 70 | 5 / 8 |
| 80 — 120 | 4 | 40 — 90 | 5 / 6 |
| 120 — 200 | 3 | 50 — 120 | 4 / 6 |
| 200 — 400 | 2 | 80 — 180 | 3 / 4 |
| 300 — 700 | 1.25 | 130 — 350 | 2 / 3 |
| over 600 | 0.75 | 220 — 600 | 1.5 / 2 |
| Recommended tooth pitch for cutting tubes | |||||||||||
| Wall thickness, mm |
Tube diameter, mm Tooth pitch, Z |
||||||||||
| 20 | 40 | 60 | 80 | 100 | 120 | 150 | 200 | 300 | 500 | ||
| 2 | 14 | 10 / 14 | 10 / 14 | 10 / 14 | 10 / 14 | 8 / 12 | 8 / 12 | 8 / 12 | 8 / 12 | 5 / 8 | |
| 3 | 14 | 10 / 14 | 10 / 14 | 8 / 12 | 8 / 12 | 8 / 12 | 8 / 12 | 6 / 10 | 6 / 10 | 5 / 8 | |
| 4 | 10 / 14 | 10 / 14 | 8 / 12 | 8 / 12 | 8 / 12 | 6 / 10 | 6 / 10 | 5 / 8 | 5 / 8 | 4 / 6 | |
| 5 | 10 / 14 | 10 / 14 | 8 / 12 | 8 / 12 | 6 / 10 | 6 / 10 | 5 / 8 | 4 / 6 | 4 / 6 | 4 / 6 | |
| 6 | 10 / 14 | 8 / 12 | 8 / 12 | 6 / 10 | 6 / 10 | 5 / 8 | 5 / 8 | 4 / 6 | 4 / 6 | 4 / 6 | |
| 8 | 10 / 14 | 8 / 12 | 8 / 12 | 6 / 10 | 5 / 8 | 5 / 8 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | |
| 10 | — | 8 / 12 | 6 / 10 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 5 | |
| 12 | — | 8 / 12 | 6 / 10 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 5 | |
| 15 | — | 8 / 12 | 6 / 10 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 5 | 4 / 5 | 4 / 5 | |
| 20 | — | — | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 6 | 4 / 5 | 4 / 5 | 4 / 5 | 3 / 4 | |
| 30 | — | — | — | 4 / 6 | 4 / 6 | 4 / 5 | 4 / 5 | 4 / 5 | 4 / 5 | 2 / 3 | |
| 50 | — | — | — | — | — | — | 4 / 5 | 3 / 4 | 2 / 3 | 2 / 3 | |
- Saw blade width
It is recommended to use blades of the maximum possible width. The wider the blade, the more stable the operation at high feed rates. When cutting curves, blade width limits the minimum cutting radius.
| Radius, mm | 3 | 8 | 15 | 30 | 38 | 65 | 100 | 140 |
| Blade width, mm | 3 | 5 | 6 | 8 | 10 | 13 | 16 | 20 |
Product reviews
All MELITA reviews →- Андрей П.Purchase via Prom.ua
Similar items: Metal-cutting band saws
Entire category →
● In stockMetal band saw OPTIsaw S 275P
power1.1 kWvoltage400 Vweight185 kg
109 680 ₴incl. VAT · 91 400 ₴ excl. VAT

● In stockMetal-cutting band saw PPK-200U
voltage400 Vweight150 kg
99 600 ₴incl. VAT · 83 000 ₴ excl. VAT